Controlled handling
Maintain product position and separation through inspection and packaging.
01Medical & life sciences
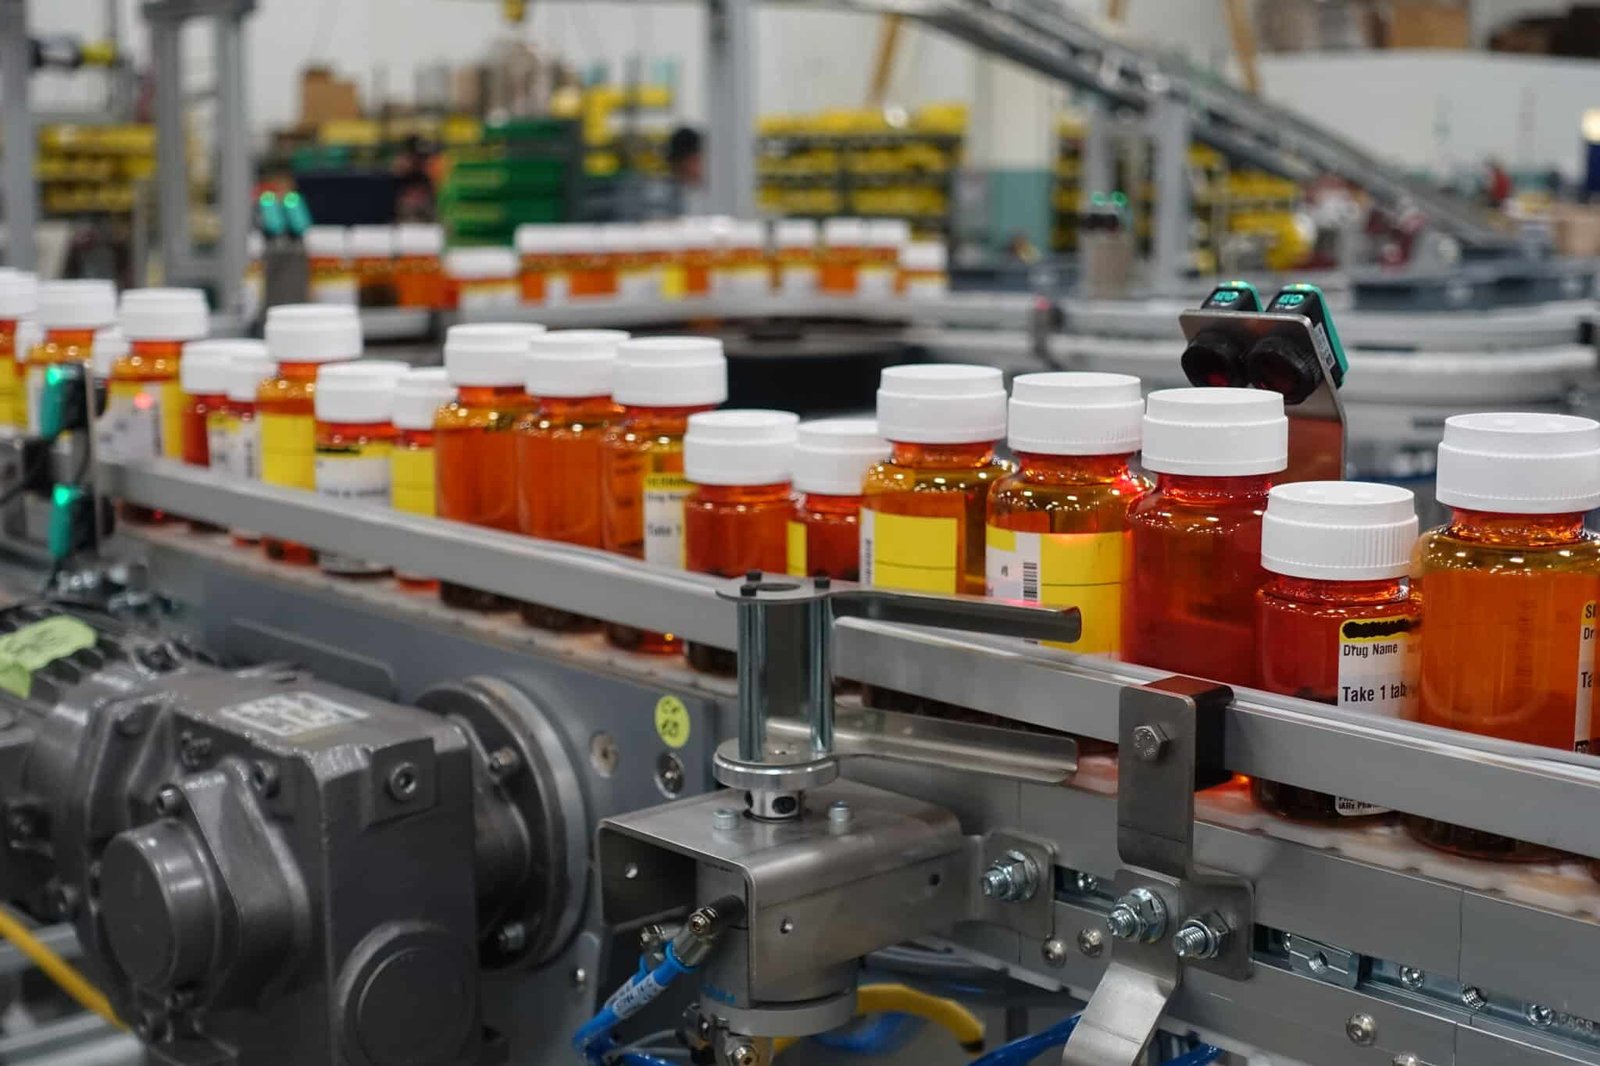
Pharmaceutical conveyors control bottles, blister packs, totes and components through manufacturing, inspection, filling, labelling, packaging and accumulation.
02Handling challenges
The conveyor layout, surface, guides and controls should be selected around the real product, transfer points and operating environment.
Maintain product position and separation through inspection and packaging.
Match conveyor materials and access to the hygiene needs of the process area.
Route totes and packs through defined production and quality-control steps.
03Applications
These are representative uses documented for this industry; the final arrangement depends on product trials and line requirements.
04Relevant platforms
Explore the Roarer platform pages that most closely match the handling conditions described in the source material.
05Related solutions
Positioning, inspection, routing and flow-control solutions can be integrated around the selected conveyor platform.
06Related industries
07Application review
Share the product, environment, throughput and transfer requirements. Roarer will help define an appropriate conveyor approach.