01
Practical overview
Prioritizing product quality is essential for companies to ensure consumer safety, meet government regulations, avoid costly recalls, and build trust.
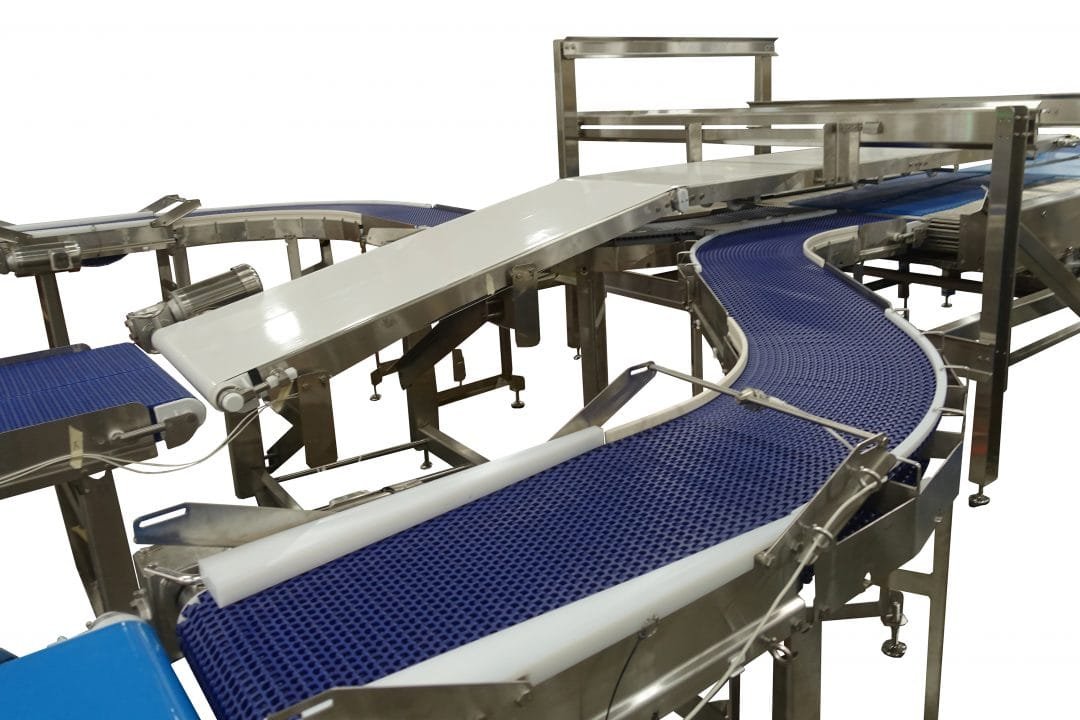
Manufacturers must implement thorough inspection processes, and automating these procedures with conveyors can transform your quality control measures.
02
Why Maintaining High Quality Standards is Critical Across Industries
Strict quality standards are crucial across manufacturing sectors, but this is especially true in highly regulated industries such as pharmaceuticals, food processing, and cosmetics. By upholding high quality standards, the operation will:
When defective products make it to market, massive recalls often follow. In the food industry, for example, heightened inspection can help detect contaminants, spoilage, or other defects, thus helping to maintain product quality and preventing meat and produce recalls that damage consumer trust.
High standards, coupled with thorough inspection processes, reduce recall risk and associated costs.
Consumers rely on quality standards to remain safe. From spoiled food to damaged blister packs, faulty products can have serious health consequences for consumers. High standards reduce the number of safety issues like spoiled food, damaged packaging, or defective electronics that could harm consumers.
03
Competitive Advantages of Automating Your Product Inspection Process
Manually inspecting products is a time-consumer and error-prone process. By automating some elements of product inspection, operators can gain the following benefits:
Automating product inspection can help minimize wasted materials and resources by improving the process of identifying defects and isolating flawed products.
Efficiency improves when your inspection process isn’t a bottleneck. With conveyor systems, operators can be able to move, sort, and inspect products more quickly and with minimal errors, increasing your efficiency and overall productivity.
Automation also increases throughput, freeing your staff for more strategic tasks.
04
Backlit Industrial & Sanitary Conveyors
Conduct more detailed inspections with backlit conveyor belts.
In food processing and pharmaceutical manufacturing, ensuring product quality and consumer safety is key.
Inevitably, some products on your line will not be fit for distribution. Through product inspection, operators can be able to efficiently sort out items that can’t be sold or consumed, improving your overall product quality and keeping consumers safe and happy.
Whether you’re in the pharmaceutical, food processing, or other heavily-regulated industries, ensuring your product inspection process runs smoothly and efficiently should be a top priority.